Modern manufacturing demands faster, more reliable quality checks at every stage of production. As part complexity grows and tolerances tighten, inspection teams need structured workflows that connect raw measurement data to clear, defensible decisions. Here is how 3D metrology software reshapes that process from first scan to final report.
Connects scan and CMM data to repeatable inspection steps and clearer decisions.
Reduces rework by standardizing alignment, GD&T evaluation, and reporting.
Improves traceability and collaboration across quality, production, and suppliers.
1) From raw 3D data to actionable inspection decisions
A typical 3D inspection workflow follows five repeatable stages: acquisition, alignment, feature extraction, tolerance evaluation, and reporting. Each stage builds on the previous one, which means errors introduced early compound downstream. Understanding the full chain helps teams intervene at the right point rather than chasing symptoms at the end.
Data acquisition and quality of input
Higher point density does not automatically improve accuracy, because measurement uncertainty is driven by the sensor, setup, and calibration. A dense point cloud captured with poor fixturing or in an unstable thermal environment will produce misleading results regardless of nominal resolution.
Practical capture strategy matters: plan coverage to avoid occlusions, prepare surfaces to minimize reflectivity issues, and calibrate instruments before each session. The choice of sensor, whether a CMM, laser scanner, structured light system, or CT scanner, should match the geometry and tolerance range of the part, not just what is available on the floor.
Alignment, datums, and tolerance logic
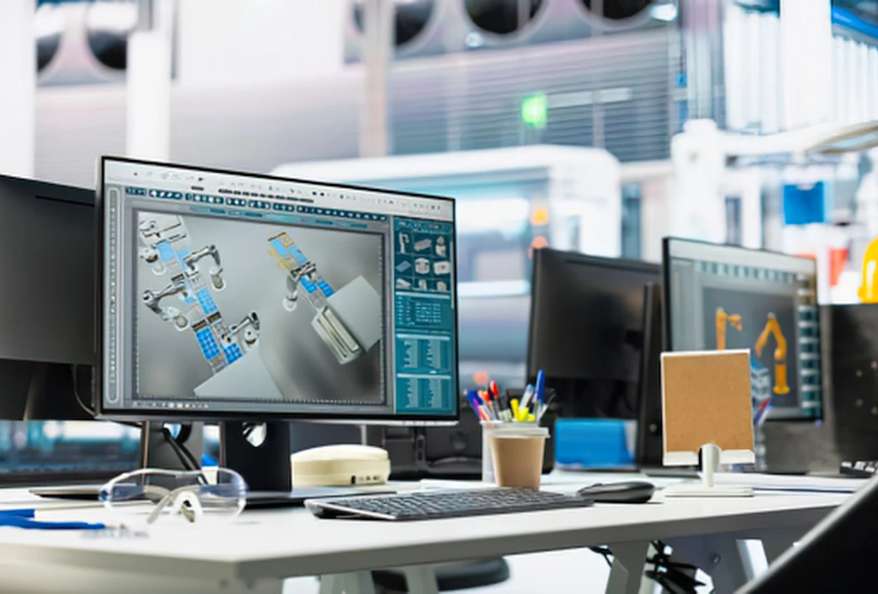
Datum-based alignment is the default for functional GD&T verification because it mirrors how parts assemble in real products. Using 3D metrology software helps teams move from scan data to standardized GD&T checks and reports, enforcing the correct datum scheme consistently across operators and shifts.
Best-fit alignment has its place in freeform surface comparison and reverse engineering, but it is risky for acceptance decisions because it can absorb real deviations into the alignment itself. Feature extraction, pulling planes, circles, and slots from the point cloud, feeds directly into tolerance evaluation. The software then computes actual versus nominal values and flags out-of-tolerance conditions.
Reporting that supports decisions
A good inspection report must be traceable to the part revision, the measurement plan, and the instrument used. Without that traceability, a report is a snapshot with no audit trail.
Effective reports include part ID, revision level, datum definitions, tolerances, measured results, operator identity, and timestamp. Outputs should be tailored to the audience: a shop-floor team needs a quick pass/fail summary, while a QA sign-off package requires full feature tables, color deviation maps, and supporting metadata.
2) Workflow gains: repeatability, speed, and fewer quality escapes
Standardized inspection templates reduce operator-to-operator variation by enforcing the same alignment, feature definitions, and tolerance rules each run. This consistency is the foundation for comparing results across shifts, sites, and time periods without questioning whether differences reflect real part variation or measurement method differences.
Reducing variability across shifts and sites
Repeatability in inspection is as much about consistent methods as it is about instrument capability. Embedding work instructions directly into the software, including datum selection, probing strategy, and acceptance criteria, removes interpretation from the operator and locks in the intended method.
Version control of inspection programs is equally important. When a CAD model is updated, the corresponding measurement plan must be reviewed and updated in a controlled way. Unmanaged changes silently invalidate historical comparisons.
Faster root-cause analysis with 3D context
Full-field 3D deviation maps can reveal deformation patterns that single-point measurements may miss. A color map showing systematic warpage across a molded panel, for example, points directly to a process issue rather than a random defect.
This spatial context accelerates root-cause analysis for common manufacturing problems: springback in formed sheet metal, tool wear in machined bores, thermal distortion after heat treatment, or layer-to-layer deviation in additive parts. Linking deviation patterns to specific process steps shortens the feedback loop and reduces late-stage scrap.
Supplier quality and digital handoffs
Digital inspection outputs are most useful when they are comparable across suppliers using the same datum scheme and tolerance definitions. A report generated with a different coordinate origin or an ambiguous datum target cannot be reliably compared to an in-house result.
Define what to share with suppliers upfront: the measurement plan, report format, revision identifiers, and datum targets. Common pitfalls include mismatched coordinate systems and tolerance interpretations that differ between drawing and software settings. Resolving these at the start of a program avoids disputes at delivery.
3) Implementation checklist: what to evaluate before you deploy
Successful deployment depends on four pillars: data compatibility, validated workflows, training, and traceable documentation. Skipping any one of these creates gaps that surface later as measurement disputes or audit findings.
Choosing workflows that match your risk level
High-risk characteristics require stricter datum control and documented acceptance criteria than exploratory best-fit comparisons. Safety-critical, fit-critical, and function-critical features need a defined measurement plan, a validated method, and a clear escalation path when results are borderline.
Classify characteristics before writing inspection programs. Cosmetic features may tolerate a faster, less rigorous workflow. Functional dimensions need documented re-measure protocols, confirmation with a reference instrument if needed, and an engineering disposition process for non-conformances.
Proving the method before scaling
A pilot should end with a documented, repeatable measurement plan that multiple operators can run with consistent outputs. That is the acceptance criterion for moving from pilot to production deployment.
Scope the pilot tightly: one part family, well-defined tolerances, and a known pain point such as high rework rate or frequent supplier disputes. Run correlation checks between the new method and the existing reference. Complete operator training and validate the report sign-off workflow before expanding. Vendors such as Metrologic DCS are among those whose platforms teams may evaluate during this phase, alongside others in the market.
Integration with PLM, QMS, and MES systems should be scoped early, but avoid over-engineering the first deployment. A working, validated standalone workflow is more valuable than a partially integrated one.
Frequently asked questions about 3D metrology software
What is 3D metrology software used for in manufacturing inspection?
It converts raw measurement data from scanners, CMMs, or CT systems into measurable geometric features, evaluates them against CAD-defined tolerances, and generates traceable inspection reports. It supports first article inspection, in-process checks, and final acceptance across a wide range of industries.
How is 3D scanning inspection different from a traditional CMM workflow?
A CMM measures discrete points defined in a measurement plan. 3D scanning captures full-surface point clouds, enabling deviation maps and analysis of features not anticipated during planning. Both approaches require proper alignment and calibration; they are often used together rather than as alternatives.
When should you use best-fit alignment versus datum alignment?
Use datum alignment for any acceptance decision tied to functional GD&T requirements. Best-fit is appropriate for freeform surface comparison, reverse engineering, or exploratory analysis where no functional datum scheme is defined. Mixing the two without documentation creates ambiguity in results.
What should a traceable 3D inspection report include?
At minimum: part number and revision, datum definitions, nominal and measured values for each characteristic, tolerance limits, pass/fail status, instrument identification, operator name, and date. This information allows the report to be reconstructed, audited, or compared against future measurements.
Shreyas Kulkarni is a Chartered Electrical Engineer and renewable energy pioneer with over eight years of hands-on experience in the clean energy sector. He is the Co-Founder of UNICUS Energy, a leading provider of solar energy solutions in India, where he drives technical execution, system architecture, and clean tech deployment.
As an author for ENTECH Magazine, Shreyas focuses on making solar technology practical and understandable for students, engineers, and homeowners. His contributions include detailed guides on the inner workings of rooftop solar systems and deep dives into modern hardware advancements, such as lightweight solar panels and flexible photovoltaic materials.