Every measurement carries uncertainty — an interval for example, expresses how much doubt surrounds the result.
How to Calculate Uncertainty in Measurement Like a Pro
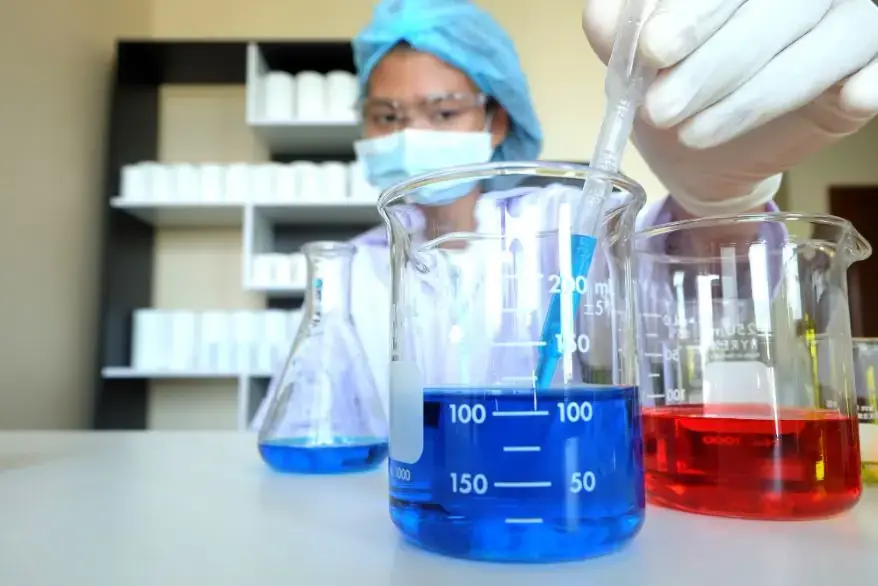
Calculate Uncertainty in measurement, in fact, is the quantified doubt associated with a measurement result. However, it is not a mistake you made. Rather, it is an honest statement of the range within which the true value of the measure quantity is expect to lie.
Every instrument has a resolution limit, every method has assumptions, as well as every environment changes. Uncertainty is the disciplined way of accounting for those limits so that a result can be trusted, compared, and reproduced.
Key takeaways: Calculate Uncertainty in Measurement
- Every measurement carries uncertainty — an interval for example, expresses how much doubt surrounds the result.
- The international authority is the GUM (JCGM 100:2008). It uses Type A as well as Type B evaluations, a combined standard uncertainty (uc), and an expanded uncertainty (U = k × uc).
- Always build an uncertainty budget — a table that lists, quantifies, as well as combines every source of uncertainty.
- Report a result in the standard form: value ± U, together with the coverage factor k and the confidence level.
Also Read: Analytical Chemistry
What Is Uncertainty in Measurement?
Two related ideas are frequently confused, and separating them is the foundation of correct uncertainty analysis:
- Error vs. uncertainty. An error is the (usually unknowable) difference between the measured value and the true value. Uncertainty is the doubt that remains about the result after you have done your best measurement. You can rarely state the error exactly, but you can quantify the uncertainty.
- Accuracy vs. precision. Accuracy is closeness to the true value; precision is the scatter among repeated measurements. A result can be precise but biased (systematically wrong), or accurate on average but imprecise. Uncertainty analysis must consider both.
Why Calculate Uncertainty in Measurement Matters
Without a stated uncertainty, a measurement is just a number with no meaning. Consider these real consequences:
- Metrology and industry. A “test uncertainty ratio” (TUR) compares your measurement system’s expanded uncertainty to the tolerance of the part you are checking. A common acceptance rule is TUR ≥ 4:1 — the measurement uncertainty should be no more than one-quarter of the tolerance band. A low TUR means you cannot reliably decide whether a product passes or fails.
- Analytical chemistry and health. When a laboratory reports a blood concentration or a contaminant level, the result decides a diagnosis, a compliance ruling, or a recall. ISO/IEC 17025 requires accredited laboratories to estimate and report measurement uncertainty.
- Science and forecasting. Edward Lorenz’s work on deterministic chaos — the “butterfly effect” — showed how tiny uncertainties in initial conditions can grow into large differences in a forecast. Quantifying uncertainty is how scientists bound that growth.
In short: a measurement result without an uncertainty estimate is incomplete.
The Standard to Follow: GUM and Its Terminology
For consistency across laboratories and countries, metrologists follow the “Guide to the Expression of Uncertainty in Measurement” (GUM), published as JCGM 100:2008 (and issued earlier as ISO/IEC Guide 98-3). For analytical chemistry specifically, the companion guidance is the EURACHEM/CITAC Guide CG 4, “Quantifying Uncertainty in Analytical Measurement.”
The GUM introduces two ways of evaluating uncertainty — note that these are types of evaluation, not types of error:
- Type A evaluation — uncertainty estimated from the statistical analysis of repeated observations (for example, the standard deviation of the mean of ten readings).
- Type B evaluation — uncertainty estimated by any other means: calibration certificates, manufacturer specifications, reference data, or documented experience (for example, taking an instrument’s ±0.5 mL tolerance and converting it to a standard uncertainty using a probability distribution).
The older language of “random” and “systematic” errors still describes why results scatter or shift, but the GUM’s Type A/Type B terminology gives you a consistent recipe for turning each source into a number.
Expert tip: this article deliberately uses the GUM’s terms — standard uncertainty (u), combined standard uncertainty (uc), coverage factor (k), and expanded uncertainty (U) — so that your uncertainty budget is directly comparable with ISO/IEC 17025 reports and published metrology data.
Step 1 — Define the Measurand and Write the Measurement Model
Before calculating anything, state exactly what you are measuring (the measurand) and how the result depends on the inputs.
Write a simple model equation. For a direct measurement, the model may be trivial:
V = reading
For a calculated quantity, the model shows the relationship. Example — calculating density from mass and volume:
ρ = m / V
The model matters because it determines each input’s sensitivity coefficient (ci), which you will use in Step 4.
Step 2 — Identify All Sources: Calculate Uncertainty in Measurement
List every factor that could move the result away from the true value. Group them so nothing is double-counted:
- Instrument — Firstly, instrument-related factors include resolution, calibration tolerance, drift, and ageing.
- Method — Additionally, method-related factors involve repeatability, recovery, extraction efficiency, and assumptions within the model.
- Environment — Meanwhile, environmental conditions, such as temperature, humidity, pressure, vibration, and electromagnetic interference, can also influence measurement results.
- Operator — Furthermore, operator-related factors include reading a scale or meniscus, timing, and maintaining a consistent technique.
- Reference/material — Finally, the purity of reagents, certified reference values, and sample homogeneity can also contribute to measurement uncertainty.
“Errors using inadequate data are much less than those using no data at all.” — Charles Babbage
Step 3 — Quantify Each Source (Type A and Type B)
Type A evaluation (from repeated measurements)
- Take n repeated readings: x1, x2, … xn.
- Calculate the mean:
x̄ = (Σ xi) / n - Calculate the sample standard deviation:
s = √[ Σ(xi − x̄)² / (n − 1) ] - The standard uncertainty of the mean is:
u(x̄) = s / √n
The more repeats you take, the smaller u(x̄) becomes — this is the statistical way to shrink uncertainty.
Type B evaluation (from a stated limit or tolerance)
When only a limit ±a is given (a calibration tolerance, a manufacturer’s accuracy, a handbook range), convert it to a standard uncertainty by dividing by a divisor that depends on the assumed probability distribution:
| Distribution | Divisor | When to use it |
|---|---|---|
| Rectangular (uniform) | √3 ≈ 1.73 | Only the limits ±a are known; any value inside is equally likely |
| Triangular | √6 ≈ 2.45 | Values near the centre of ±a are more likely |
| Normal, k = 2 | 2 | A calibration certificate states the uncertainty at ~95% confidence |
| Normal, k = 3 | 3 | A certificate states the uncertainty at ~99% confidence |
For example, a balance with a stated accuracy of ±0.5 mg, treated as rectangular, contributes u = 0.5 / √3 ≈ 0.29 mg.
Step 4 — Combine into the Combined Standard Uncertainty (uc)
Once every source is a standard uncertainty in the same units, combine them using the law of propagation of uncertainty:
uc² = (c1·u1)² + (c2·u2)² + (c3·u3)² + …
where ci is the sensitivity coefficient of each source (how much the final result changes per unit change in that input).
The shortcut most people recognise — the root-sum-of-squares (RSS) formula — is the special case where every ci = 1:
uc = √(u1² + u2² + u3² + …)
RSS assumes the sources are independent (uncorrelated). If two sources share a common cause — for example, two readings affected by the same room temperature — you may need to account for correlation; in most practical budgets, independence is a reasonable first assumption.
Step 5 — Calculate the Expanded Uncertainty (U)
Most reports need a wider interval than uc, so the result carries a stated confidence level. Multiply by the coverage factor k:
U = k × uc
k = 2gives approximately a 95% confidence level (the most common choice).k = 3gives approximately a 99% confidence level.
Step 6 — Report the Result Correctly
State the result, the expanded uncertainty, the coverage factor, and the confidence level — with units:
V = 100.00 mL ± 0.64 mL (k = 2, ≈ 95% confidence)
Never report more precision than justified, and round the uncertainty to one or two significant figures (two is standard practice).
Worked Example — Measuring 100 mL in a Graduated Cylinder
Thus, You measure a nominal 100 mL volume of water in a 100 mL graduated cylinder as well as want to report the result with expanded uncertainty.
Model: V = reading (a direct measurement), so every sensitivity coefficient ci = 1.
Step 3a — Type A (repeatability). Ten readings are taken: 99.8, 100.1, 99.9, 100.2, 100.0, 99.7, 100.1, 100.0, 99.9, 100.3 mL. The mean is 100.00 mL and the sample standard deviation is s = 0.183 mL. The standard uncertainty of the mean is therefore u(rep) = 0.183 / √10 ≈ 0.058 mL.
Step 3b — Type B (specifications, environment, operator).
- Cylinder calibration: manufacturer tolerance ±0.5 mL (rectangular) →
u(cal) = 0.5 / √3 ≈ 0.289 mL. - Temperature: the lab is ±5 °C from calibration temperature; the thermal expansion of water (≈2.1 × 10⁻⁴ /°C) changes a 100 mL volume by ≈ 0.105 mL (rectangular) →
u(temp) = 0.105 / √3 ≈ 0.061 mL. - Meniscus reading: half of the 0.5 mL marking interval = ±0.25 mL (triangular) →
u(read) = 0.25 / √6 ≈ 0.102 mL.
Uncertainty budget:
| Source | Type | Estimate (±a or s) | Distribution | Divisor | Standard uncertainty u (mL) | Sensitivity c | Contribution (mL) |
|---|---|---|---|---|---|---|---|
| Repeatability (mean of 10) | A | s = 0.183 mL, n = 10 | — | √n | 0.058 | 1 | 0.058 |
| Cylinder calibration | B | ±0.500 mL | Rectangular | √3 | 0.289 | 1 | 0.289 |
| Temperature (ΔT = ±5 °C) | B | ±0.105 mL | Rectangular | √3 | 0.061 | 1 | 0.061 |
| Meniscus reading | B | ±0.250 mL | Triangular | √6 | 0.102 | 1 | 0.102 |
Step 4 — Combined standard uncertainty:
uc = √(0.058² + 0.289² + 0.061² + 0.102²) = √0.101 ≈ 0.32 mL
Thus, This is one of the important step.
Step 5 — Expanded uncertainty: U = 2 × 0.32 = 0.64 mL
Step 6 — Final reported result:
V = (100.00 ± 0.64) mL, where U = 0.64 mL at k = 2 (≈ 95% confidence).
Notably, the calibration tolerance dominates the uncertainty budget; therefore, improving repeatability alone would barely reduce the total uncertainty. Consequently, the practical value of an uncertainty budget lies in identifying where to focus improvement efforts for the greatest impact.
How to Reduce Measurement Uncertainty (and Common Mistakes)
Reduce it by design:
- Firstly, calibrate instruments according to schedule and, whenever possible, use certified reference materials.
- Additionally, control environmental conditions, including temperature, humidity, and vibration, to minimise their influence.
- Furthermore, train operators and standardise techniques, such as reading the meniscus at eye level and maintaining consistent timing.
- Moreover, increase the number of replicates, since a larger n reduces the Type A uncertainty component.
- Finally, choose a more precise instrument only when the uncertainty budget identifies it as the dominant source of uncertainty.
Avoid these common mistakes while Calculate Uncertainty in Measurement
- Firstly, Confusing error with uncertainty.
- Additionally, Mixing units or confidence levels inside one budget.
- Reporting
ucwhen the audience expects expanded uncertaintyU(or vice versa) without saying which one you used. - Dropping a source because it “looks small” — the budget is your evidence, not your guess.
- Reporting more significant figures than the uncertainty supports.
TUR check: if a part tolerance is ±1 mm and your expanded uncertainty is ±0.2 mm, TUR = 1 / 0.2 = 5:1 — acceptable under the common 4:1 rule. If TUR falls below 4:1, the measurement is not trustworthy for pass/fail decisions.
Frequently Asked Questions: Calculate Uncertainty in Measurement
What is uncertainty in measurement?
More specifically, it represents the quantified doubt associated with a measurement result, indicating the interval within which the true value is expected to lie. Importantly, it is an inherent property of every measurement, rather than an admission of failure.
What is the difference between error and uncertainty?
In contrast, error is the (usually unknowable) difference between a measured value and the true value. Uncertainty, however, represents the quantified doubt that remains around the result after measurement. Therefore, while uncertainty can be estimated, the error itself cannot be fully known.
What is the difference between Type A and Type B uncertainty?
Type A is evaluated from statistics (repeated readings). Type B is evaluated from other information — calibration certificates, specifications, reference data, or documented experience.
What is an uncertainty budget?
A table that lists every source of uncertainty, its estimated value, its probability distribution, its standard uncertainty, its sensitivity coefficient, and its contribution — then combines them into uc and U.
What is the RSS method?
RSS (root-sum-of-squares) combines independent standard uncertainties as uc = √(u1² + u2² + …). It is the special case of the GUM’s propagation formula where all sensitivity coefficients equal 1.
What is expanded uncertainty and the coverage factor?
Expanded uncertainty is U = k × uc, where the coverage factor k sets the confidence level — k = 2 for ≈95%, k = 3 for ≈99%.
What is the test uncertainty ratio (TUR)?
TUR is the tolerance of the item being measured divided by the expanded uncertainty of the measurement system. A widely used acceptance rule is TUR ≥ 4:1.
Can uncertainty be reduced?
Yes — calibrate regularly, control the environment, train operators, increase replicates, and upgrade only the dominant source in your budget.
References
- JCGM 100:2008 — Evaluation of measurement data — Guide to the expression of uncertainty in measurement (GUM), Joint Committee for Guides in Metrology / BIPM. https://www.bipm.org/documents/20126/2071204/JCGM_100_2008_E.pdf
- 3. Possolo, A. (2015). Simple guide for evaluating and expressing the uncertainty of NIST measurement results (NIST Technical Note 1900). National Institute of Standards and Technology. https://doi.org/10.6028/NIST.TN.1900
- Author
- Latest Posts
Vidisha Jain is an educator, Chemistry Subject Matter Expert, and passionate science communicator dedicated to making fundamental science engaging and accessible. She holds a Master of Science (M.Sc.) in Chemistry from Panjab University, Chandigarh, combining a strong foundation in chemical sciences with practical instructional expertise.
Currently serving as a Science Teacher at Mind Tree School, Vidisha specializes in translating complex scientific principles, chemical concepts, and laboratory dynamics into intuitive lessons for young learners. Her work focuses on fostering critical thinking, conceptual clarity, and curiosity in science classrooms, helping students bridge the gap between theoretical chemistry and real-world applications.
As an author for ENTECH Magazine, Vidisha shares insights into chemical science, effective STEM learning strategies, and classroom-tested approaches to mastering core scientific concepts.
- Author
- Latest Posts
I am an inspirational writer and emerging science blogger with a deep-rooted passion for understanding and sharing the wonders of the world around us. My journey began with a Bachelor of Science in Chemistry from AKI’s Poona College of Arts, Commerce and Science, where I developed not only a strong foundation in scientific principles but also a mindset that values curiosity, observation, and critical thinking. Studying chemistry has taught me to approach problems with logic, to look beyond the obvious, and to see patterns where others might only see complexity. These experiences have shaped the way I perceive life and influence the way I express my thoughts, both scientifically and creatively.
I have always believed that knowledge is only as powerful as the way it is shared. This belief has guided me to create content that bridges the gap between science and everyday life. I aim to simplify complex scientific ideas so they become approachable, relatable, and engaging for everyone—whether someone has a formal background in science or is simply curious about the world. Science, in my view, is not confined to textbooks and laboratories; it is a way of thinking, understanding, and connecting with the world around us. By making science accessible, I hope to inspire curiosity, ignite learning, and encourage people to see the beauty and relevance of scientific discovery in their daily lives.
Alongside my love for science, I am deeply passionate about motivational writing. I believe words carry the power to transform perspectives, encourage self-reflection, and inspire action. By combining analytical thinking with creativity, I create content that is intellectually stimulating yet emotionally resonant. Whether I am breaking down a chemical concept, exploring a scientific phenomenon, or crafting motivational narratives, my goal is to communicate ideas in a way that is clear, meaningful, and impactful.
Through my work, I strive to empower my readers – not just by helping them understand the science around them, but by inspiring them to grow, learn, and realize their full potential. Every article, post, or story I write reflects my commitment to turning knowledge into inspiration. I want to spark curiosity, encourage self-improvement, and show that learning and personal growth are deeply connected. For me, writing is not just a craft; it is a way to touch minds, connect hearts, and make ideas come alive in a way that truly resonates.